One gear, every stage in-house, photographed as it happened. This is what "cast, heat-treated and machined under one project number" actually looks like on our shop floor.
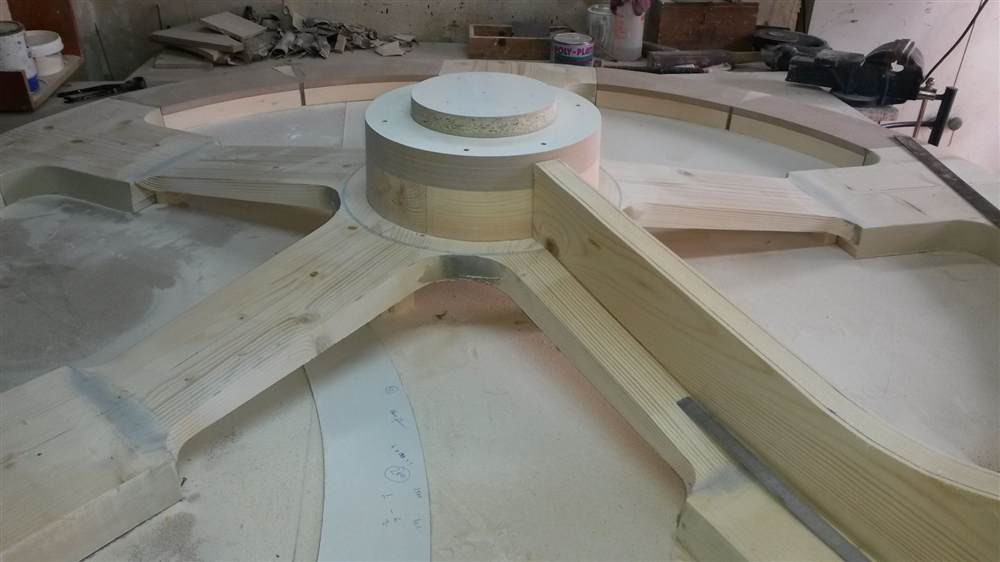
The wooden pattern is built in our pattern shop with per-alloy shrinkage allowances and per-dimension machining stock, then inspected 100% before it ever touches sand.
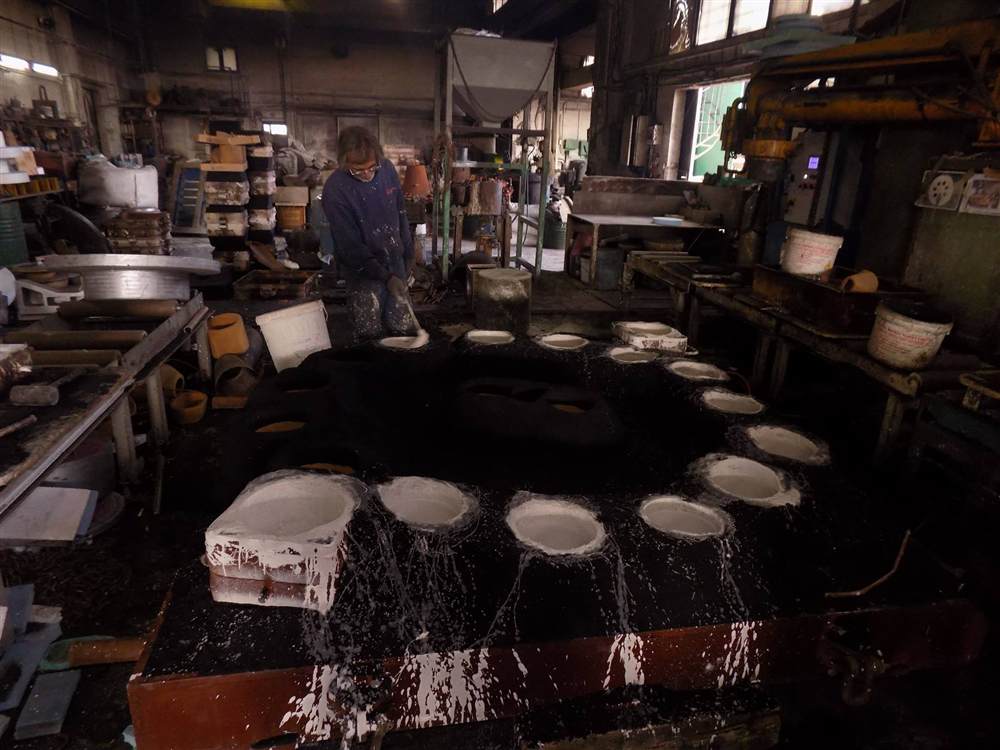
The mould is closed, coated with refractory wash and fitted with feeders sized for the section: the quiet work that decides whether a casting is sound.
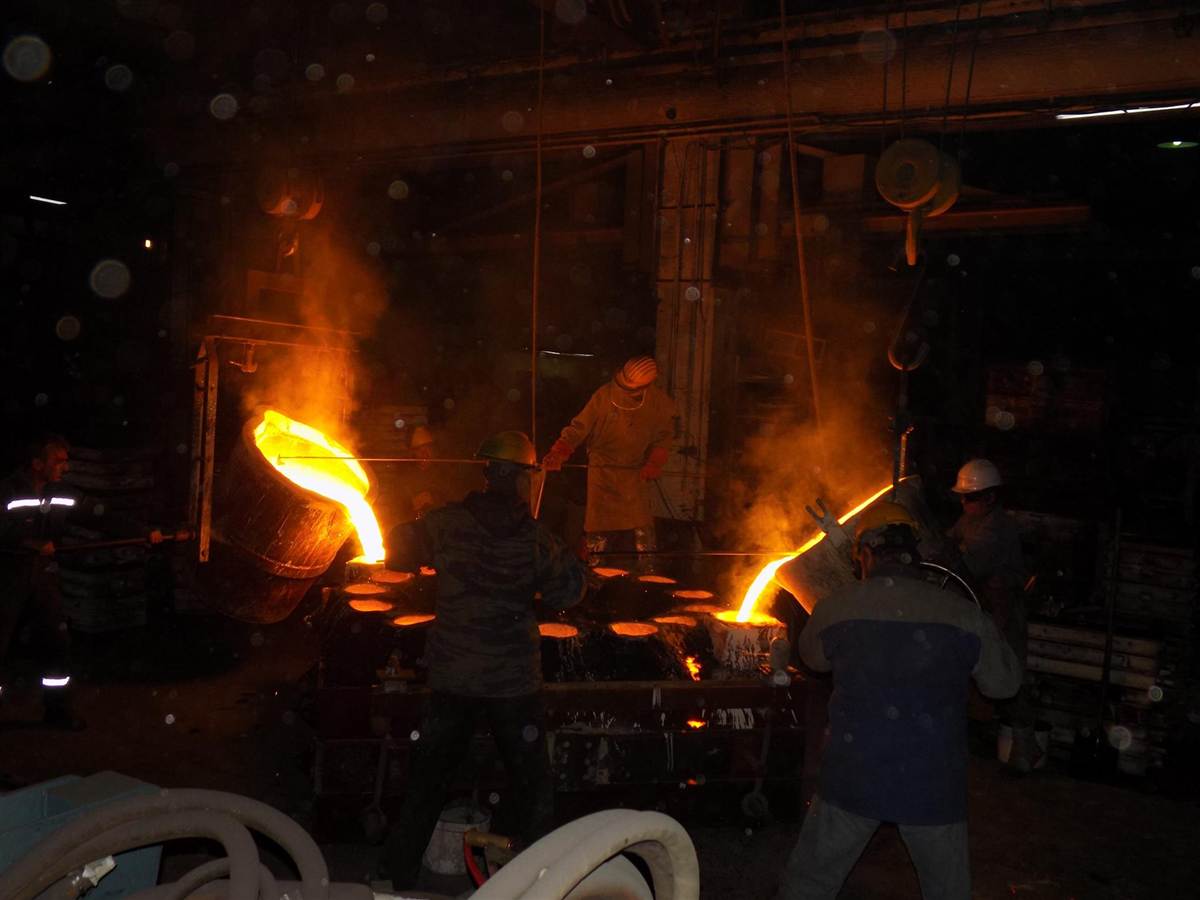
Chemistry verified by OES before the pour; temperature held within the grade's pouring range. Two ladles, one rhythm. This is the moment everything upstream was for.
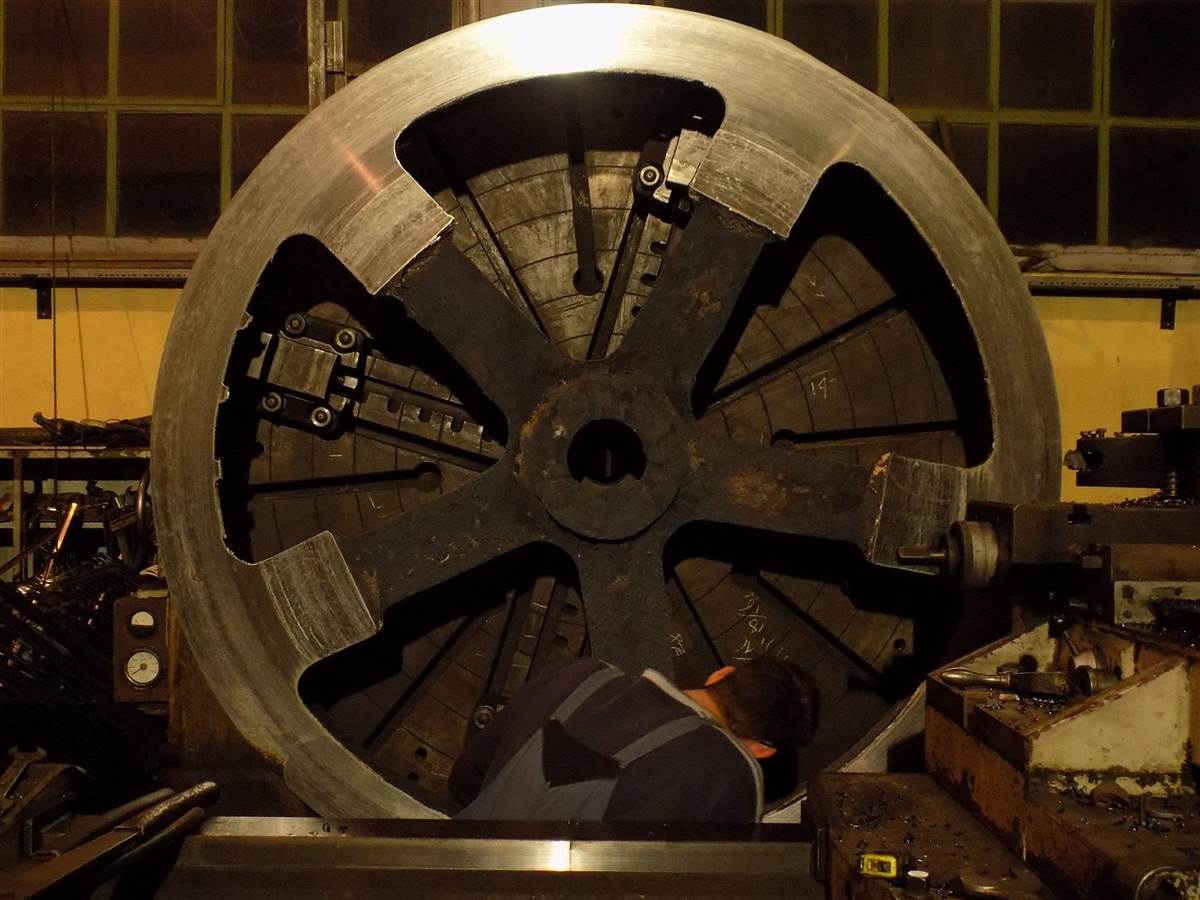
After heat treatment, the gear goes onto the lathe at our Perama machine shop and comes off at final drawing dimensions, inspected, documented, ready to install.