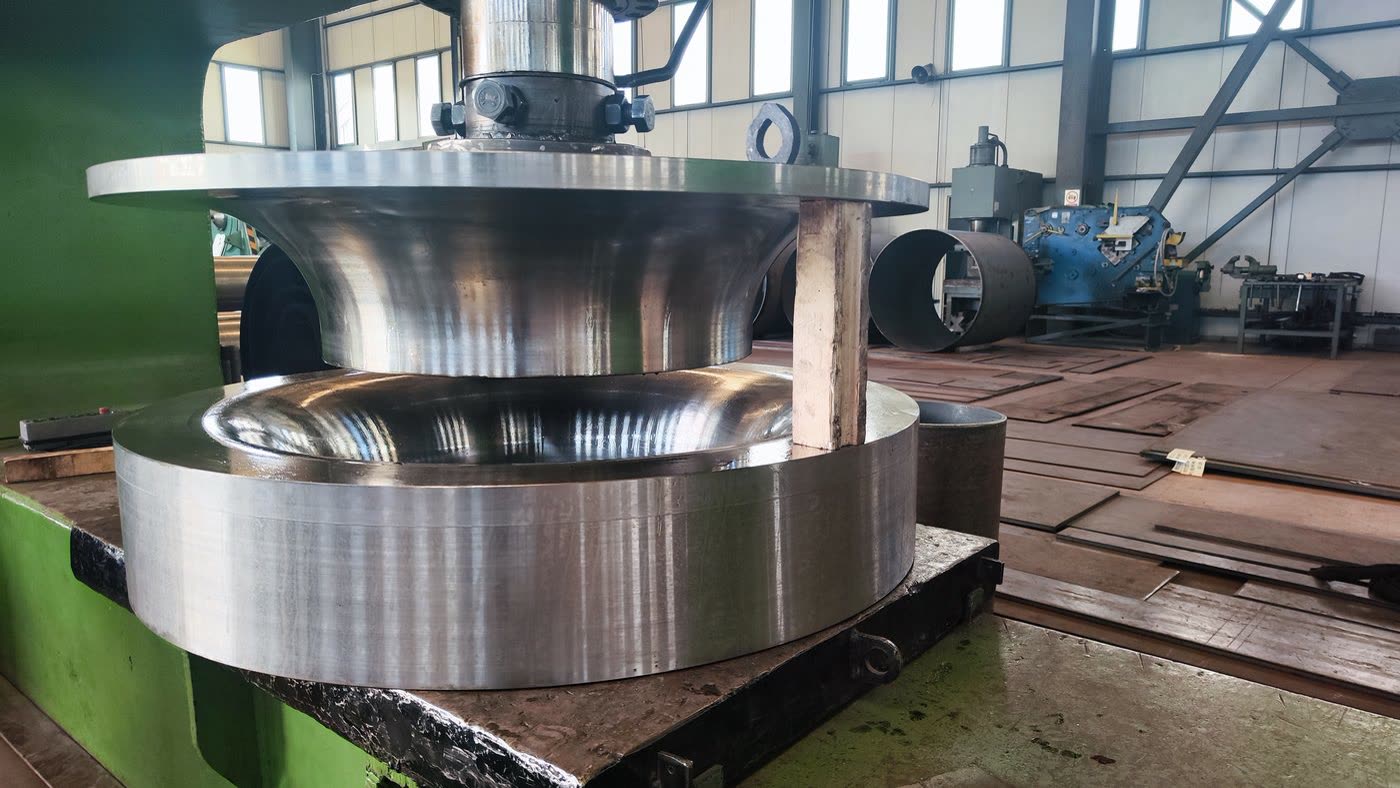
Two dedicated heat treatment furnaces on site. Heat treatment is applied to adjust mechanical properties, relieve casting stresses, or achieve the required hardness and toughness for the service application.
Equipment
Number of furnaces2 dedicated heat treatment furnaces
Solution annealing (Mn steel)1050–1070 °C · 4–6 h soak
Chrome iron cycleTwo-stage: 1020 °C/6 h + temper 280 °C/4 h
Quenching & Cooling Methods Available
Water quenching✓
Oil quenching✓
Air quenching✓
Still-air / controlled cooling✓
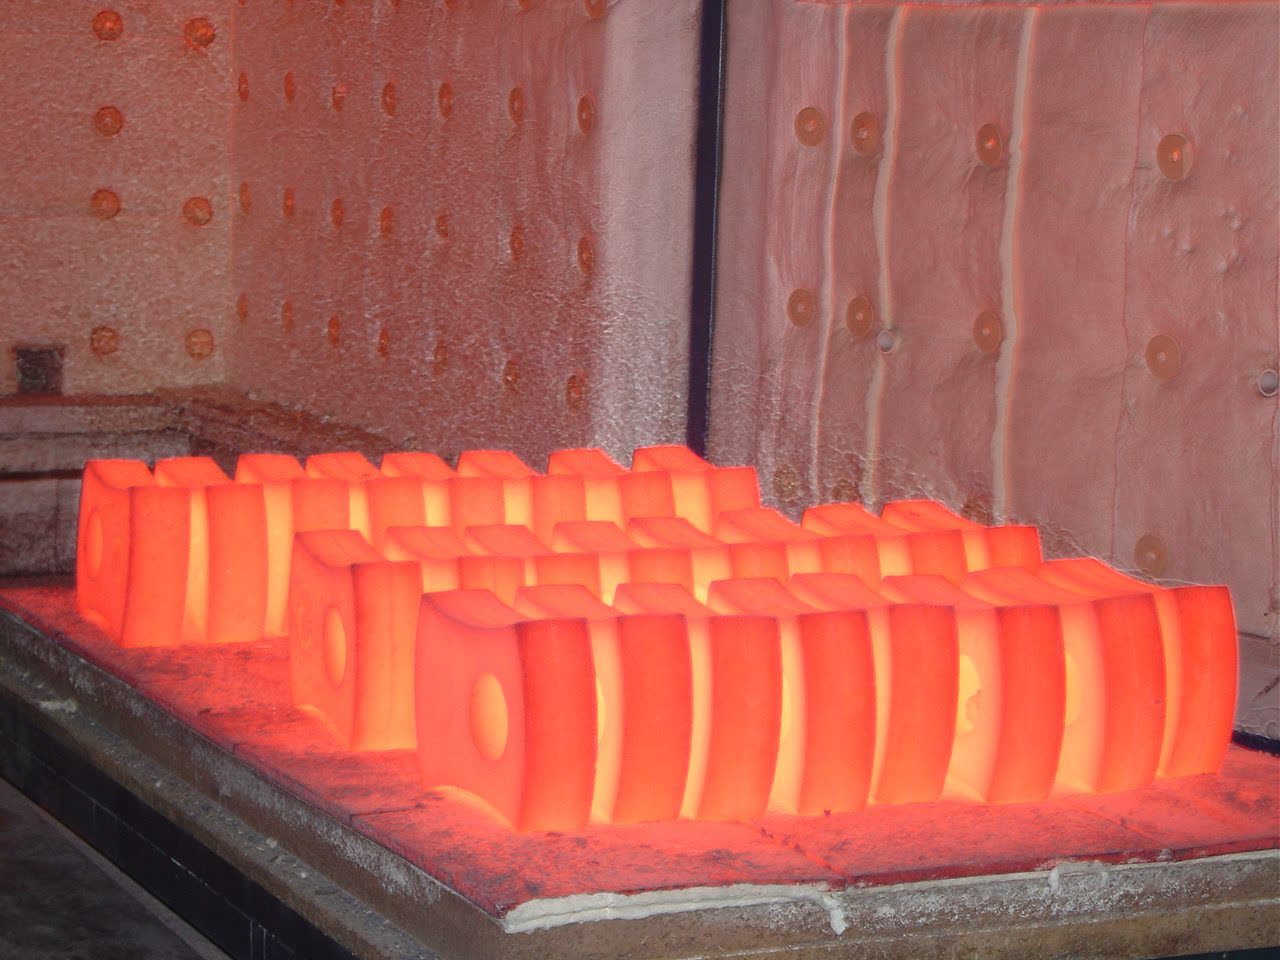
Solution annealing: manganese steel crusher hammers
Typical Heat Treatment Cycles
| Alloy | Cycle Type | Purpose | Quench Method |
|---|---|---|---|
| Manganese steel (Hadfield, GX120Mn12 family) | Solution annealing: 1050–1070 °C, 4–6 h | Dissolve carbides, achieve austenitic structure for work-hardening | Water quench with agitation |
| Steel castings | Stress relief / normalising | Reduce residual casting stresses, refine grain | Air cooling |
| Alloy steels (e.g. 42CrMo4) | Quench and temper | Achieve specified hardness and toughness | Oil or water quench + temper |
| High-chrome white iron (GX300CrMo grades) | Two-stage cycle: 1020 °C/6 h + 280 °C/4 h | Hardness ≥ 55 HRC with controlled stress state | Forced air, then still-air cooling |